




 Cart


 POPULAR CATEGORY


 ADD TO CART


| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £5.99 | 2 to 4 working days |
| Next Day | £15.54 |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 5 to 7 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
Product Number: 15089
The SIP 15089 tungsten electrode. TIG welding electrode. 4mm Ceriated Tungsten Electrode is a versatile TIG welding electrode made from high-quality ceriated tungsten with 2% Cerium Oxide grey tip. This electrode is suitable for a range of TIG welding applications using both AC and DC welding currents. High-quality grey-tipped 2. Compatible across the sip welding, sip tungsten electrodes welding range — check product specifications for exact model fit. In the welding trade, this product type is also known as tig tungsten or zirconiated tungsten.
Additional Information:
The SIP 2.4mm Ceriated Tungsten Electrode is a versatile TIG welding electrode made from high-quality ceriated tungsten with 2% Cerium Oxide grey tip.
This electrode is suitable for a range of TIG welding applications using both AC and DC welding currents.
About PartsForMachines:
PartsForMachines is a premier e-commerce platform, founded in 2019 in Warwickshire, UK, specializing in aftermarket parts and services for construction, agriculture, and industrial machinery. We offer an extensive catalog of over 500,000 products. Standard delivery: 1–3 working days within UK mainland. We are proud to be an authorised distributor, giving customers extra confidence when purchasing genuine products from us. In addition, we provide a 30-day return policy for eligible items.
| Component Type | TIG welding electrode |
|---|---|
| Manufactured From | Ceriated Tungsten (2% Cerium Oxide) |
| Engine Parts | Product Number | Product Name | Recommended Units | Product Price | |
|---|---|---|---|---|---|
|
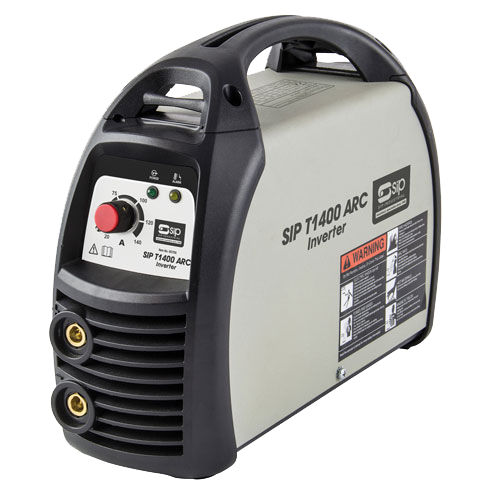
05705 | SIP 05705 T1400 ARC/TIG Inverter Welder, Input Supply - 230V, Single Phase, Output Current - 20A-140A | 1 Unit |
£122.01
£119.62
|
Add |
 Standard Delivery: £5.99
 Next Day Delivery Available
 Delivery Estimate: 2 to 4 working days
 Save Extra With 1 Offer
 Compare With Similar Items
Compare with Similar products
|
|||||||||||||||
| Technical Specification | |||||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| PRODUCT NUMBER | 02689 | 02691 | 02692 | 02693 | 02777 | 02779 | 02666 | 02668 | 02669 | 02671 | 02706 | 04000 | 04055 | 04060 | 04065 |
| Type | Electrodes | Electrodes | Electrodes | Electrodes | Electrodes | Electrodes | Welding Wire | Welding Wire | Welding Wire | Welding Wire | Welding Wire | Welding Wire | Welding Wire | Welding Wire | Welding Wire |
| Size | 1.60mm | 2.00mm | 2.50mm | 2.50mm | 4.00mm | ||||||||||
| Weight | 5kg | 5kg | |||||||||||||
| Dia | 1.60mm | 2.00mm | 2.50mm | 2.50mm | 4.00mm | 0.6mm | 0.6mm | 0.8mm | 0.8mm | 0.8mm | 0.6mm | 0.8mm | 0.8mm | 0.8mm | |
| Pack Qty | 10 | 10 | 10 | ||||||||||||
| Reel | 5kg | 5kg | 5kg | 15kg | 5kg | 15kg | 4.5kg | 0.7kg | 0.22kg | 0.5kg | 0.7kg | ||||
| Size Range | Up to 10mm | Up to 10mm | Up to 10mm | Up to 10mm | Up to 10mm | ||||||||||
| Wire | Gasless/Flux | Gasless/Flux | |||||||||||||
| Show More | |||||||||||||||
A. Compatible with: CROSARC CAP0936 and CAP0980 (and 3 more); Clarke MIG200 and 220A; Draper 70052 and 70057 (and 2 more); SIP 05705 and 05732 (and 31 more) Any TIG welder that accepts 2.4mm diameter tungsten with the appropriate collet will use this electrode.
A. Yes — ceriated tungsten is the most popular choice for DC TIG welding of mild steel, stainless steel, and most other materials. It provides reliable arc starts and a stable pointed geometry throughout the welding session.
A. 2.4mm diameter tungsten is typically used from about 100–250A. For lower-amperage work, step down to 1.6mm or 2.0mm tungsten. For higher-amperage work above 150A, step up to 3.2mm tungsten. Always stay within the amperage range for your tungsten diameter to prevent tip damage.
A. For AC TIG welding of aluminium (zirconiated tungsten), allow the tip to form a natural ball during welding — do not grind to a point. The balled tip provides stable arc ignition and holds its shape better than other types. For DC TIG welding of steel and stainless (ceriated or thoriated tungsten), grind to a pointed tip — a taper of 2 to 2.5x the electrode diameter, ground lengthwise along the rod. A correctly prepared tungsten gives clean, consistent arc starts and precise weld control.
A. Replace or re-grind when: the tip becomes contaminated (black or green discolouration), the arc starts wandering or splitting, or the tip has cracked or cratered. For DC steel work, re-grind at the first sign of arc instability — a sharp, clean tip is essential for precise TIG work.
A. The SIP 15089 pack contains 10 x 2.4mm tungsten electrodes. With careful handling and proper grinding technique, a single tungsten can last for several welding sessions. Keep spares — tungsten is brittle and a dropped electrode will often crack even if it looks undamaged.
A. No — ceriated tungsten is a DC type and is not recommended for AC aluminium welding. For aluminium, use zirconiated tungsten (also available in the TIG Consumables section), which handles the AC waveform and forms the characteristic balled tip correctly.
A. You need a 2.4mm collet and matching collet body for your TIG torch. Collets are size-specific — a 1.6mm collet will not grip 2.4mm tungsten securely. The full range of TIG collets for SR-series and compatible torches is available in the TIG Consumables — Collets section.
A. Check your machine's specification for the accepted wire diameter range (typically 0.6mm-1.2mm for MIG) or electrode diameter range (typically 1.6mm-4.0mm for ARC/MMA). The machine's output amperage determines the maximum electrode size it can run — higher amperage machines handle thicker electrodes.
A. If your TIG welder is DC or AC/DC (and you are welding steel, stainless, copper or other non-aluminium materials), the SIP 15089 is the correct tungsten type. Confirm the 2.4mm diameter matches your available collet set and your required amperage range.
By sharing your email, you agree to our privacy policy & terms of service
 Question about this product? Click here


