




 Cart


 POPULAR CATEGORY


 ADD TO CART


| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £4.99 | 2 to 4 working days |
| Next Day | £15.54 |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 5 to 7 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
Product Number: 10233
The SIP 10233 welding electrode — Amperage : 400A. The SIP 50mm² 400A Large Dinse Electrode (also known as welding rod, mma electrode or arc welding electrode) Lead is designed for heavy-duty use and long life with several quality SIP ARC welders and inverters. Reference your SIP manual for more information. 5mtr 50mm² large dinse electrode lead; 400A max. Compatible across the sip welding, sip arc electrodes welding range — check product specifications for exact model fit. In the welding trade, this product type is also known as mild steel electrode or stainless steel electrode.
Additional Information:
The SIP 50mm² 400A Large Dinse Electrode Lead is designed for heavy-duty use and long life with several quality SIP ARC welders and inverters. Reference your SIP manual for more information.About PartsForMachines:
PartsForMachines is a premier e-commerce platform, founded in 2019 in Warwickshire, UK, specializing in aftermarket parts and services for construction, agriculture, and industrial machinery. We offer an extensive catalog of over 500,000 products. Standard delivery: 1–3 working days within UK mainland. We are proud to be an authorised distributor, giving customers extra confidence when purchasing genuine products from us. In addition, we provide a 30-day return policy for eligible items.
| ITEM NO | 10233 |
|---|---|
| Amperage | 400A |
| Cable Size | 50mm² |
| Connection | Large Dinse |
| Cable Length | 5 metres |
| Pack Gross (g) | 1000 |
| Engine Parts | Product Number | Product Name | Recommended Units | Product Price | |
|---|---|---|---|---|---|
|
05737TROLLEY | SIP 05737TROLLEY WELDMATE® AUTOPLUS 130A MIG,ARC,TIG Synergic Welder with Trolley Package | 1 Unit |
£312.84
£306.71
|
Add |
|
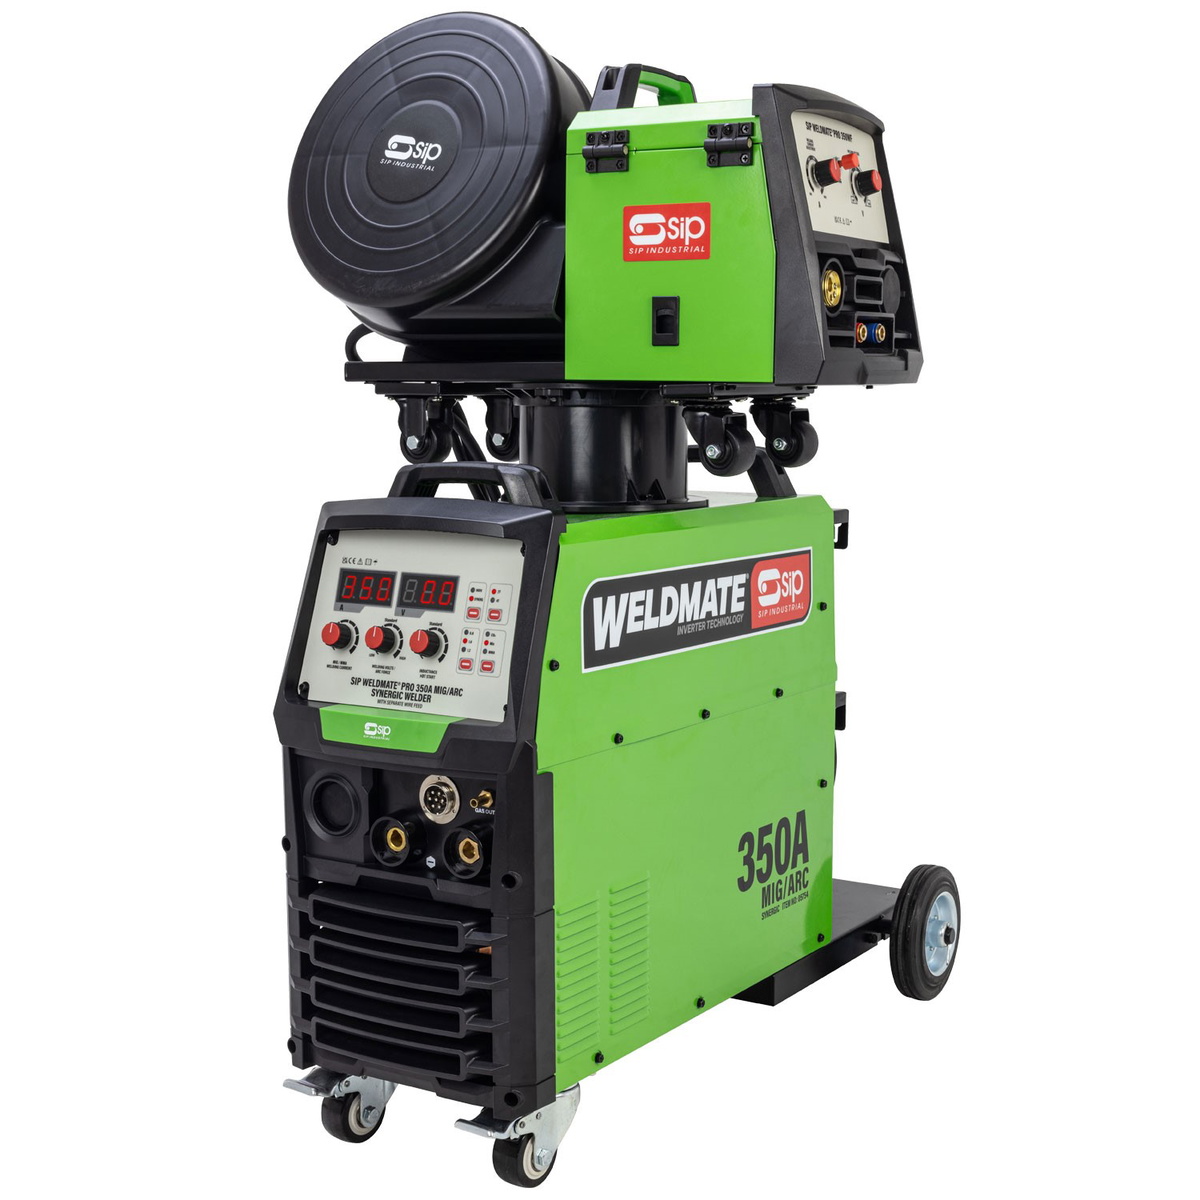
05754 | SIP 05754 WELDMATE® PRO 350A MIG/ARC Synergic Welder with Separate Wire Feed | 1 Unit |
£1,764.51
£1,729.91
|
Add |
|
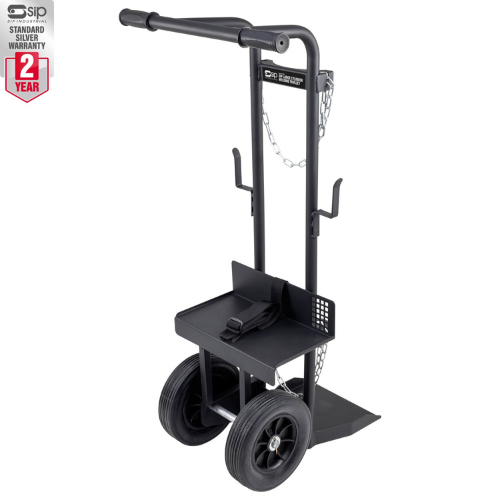
05719 | Welding Large Cylinder Trolley, 05719 SIP | 1 Unit |
£131.37
£128.79
|
Add |
|
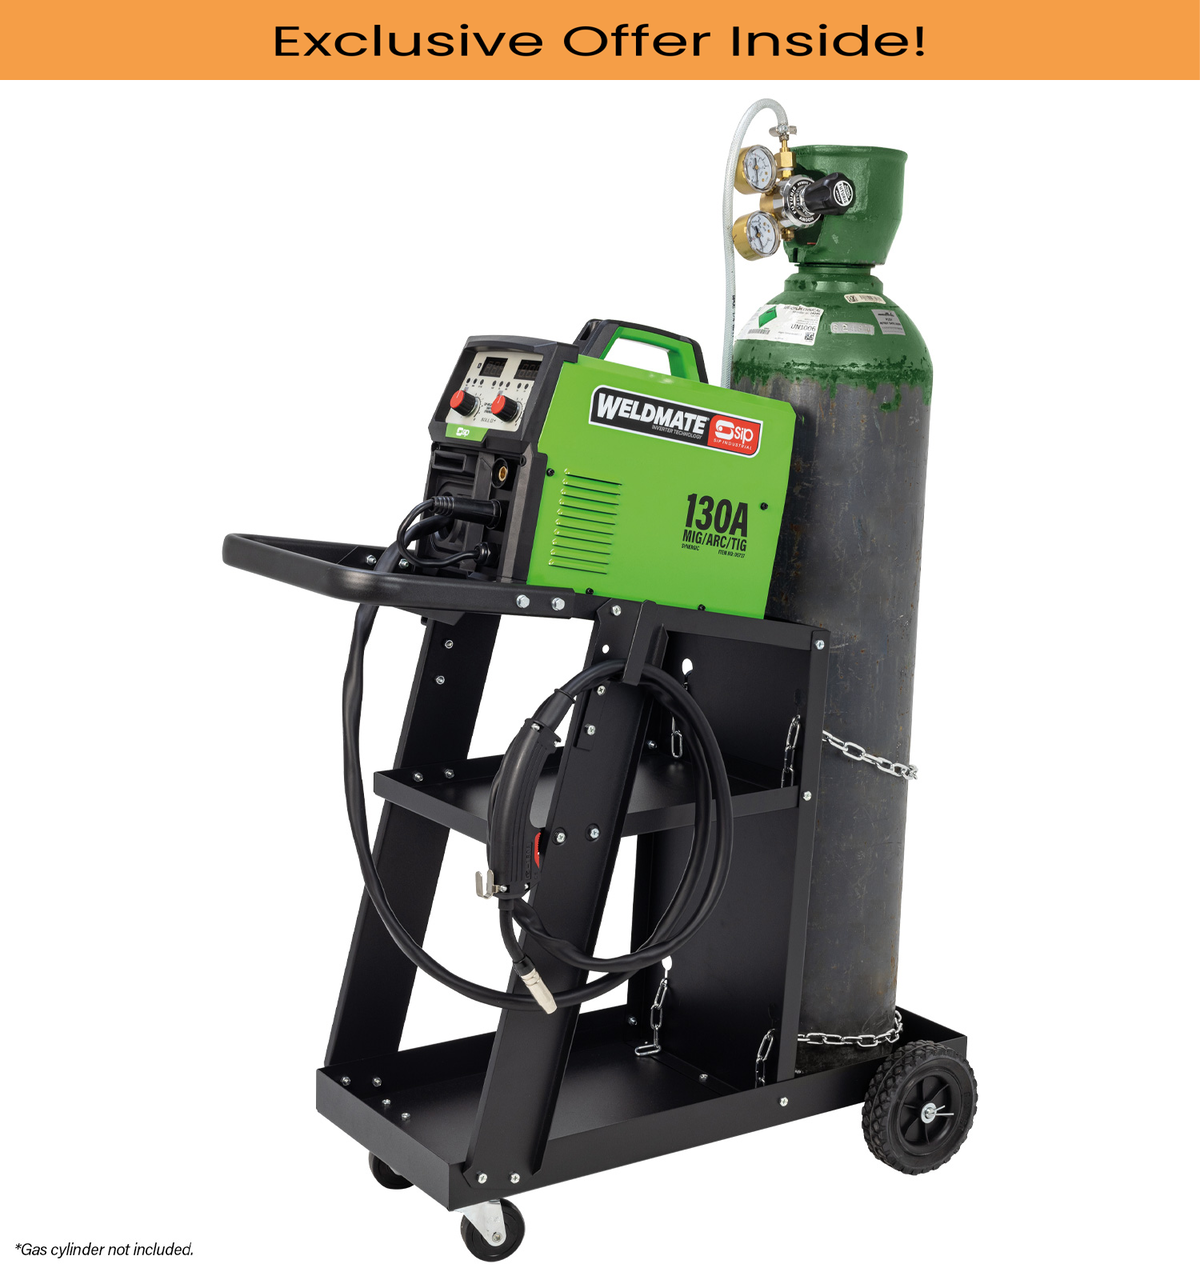
05737CART | SIP 05737CART WELDMATE® AUTOPLUS 130A MIG,ARC,TIG Synergic Welder with Cart Package | 1 Unit |
£304.81
£295.93
|
Add |

|
05737 | SIP 05737 WELDMATE® AUTOPLUS 130A MIG/ARC/TIG Synergic Welder | 1 Unit |
£262.71
£257.56
|
Add |
 Standard Delivery: £4.99
 Next Day Delivery Available
 Delivery Estimate: 2 to 4 working days
 Save Extra With 1 Offer
 Compare With Similar Items
Compare with Similar products
|
|||||
| Technical Specification | |||||
|---|---|---|---|---|---|
| PRODUCT NUMBER | 02689 | 02691 | 08372 | 29103 | 29291 |
A. The SIP 10233 is rated at 400A continuous welding current with a 50mm² cable. Ensure your machine's maximum output does not exceed this rating.
A. Compatible with all ARC/MMA welders using a large Dinse electrode socket. Check your machine's electrode terminal type matches the large Dinse connector before ordering.
A. The SIP 10233 uses a large Dinse connector. Match the connector size to your machine's electrode socket and the cable rating to your welding current.
A. Insert the large Dinse plug into the machine's electrode socket and twist to lock. Ensure the connection is firm — a loose connection causes arcing and overheating at the socket.
A. Match cable cross-section to current: 16mm² up to 160A, 25mm² up to 250A, 35mm² up to 350A, 50mm² up to 400A. This lead uses 50mm² rated at 400A.
A. Yes — a damaged lead is a common hidden cause of arc instability. Check insulation for damage, Dinse connectors for looseness, and ensure the cable rating matches your current output. Replace at any sign of damage.
A. Cable length: 5mtr. Use the shortest lead practical — longer leads increase resistance slightly. Refer to the product specification for full details, or contact PartsForMachines.com customer service for further information.
A. Yes — use a Dinse cable coupler rated to match or exceed your welding current. Ensure all connections are secure. Excess length increases resistance.
A. Check your machine's specification for the accepted wire diameter range (typically 0.6mm-1.2mm for MIG) or electrode diameter range (typically 1.6mm-4.0mm for ARC/MMA). The machine's output amperage determines the maximum electrode size it can run — higher amperage machines handle thicker electrodes.
A. Yes — UK stocked for fast despatch. Check availability at PartsForMachines.com. Orders placed before the daily cut-off are dispatched same or next working day. Check the product page for current delivery estimates.
By sharing your email, you agree to our privacy policy & terms of service
 Question about this product? Click here


