



 Cart


 POPULAR CATEGORY


 ADD TO CART



| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £4.99 | 2 to 4 working days |
| Next Day | £15.54 |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 5 to 7 working days |
| SERVICE | DELIVERY PRICE | DELIVERY TIME |
|---|---|---|
| Standard Delivery | £29.99 | 7 to 10 working days |
Product Number: 09078
Variations
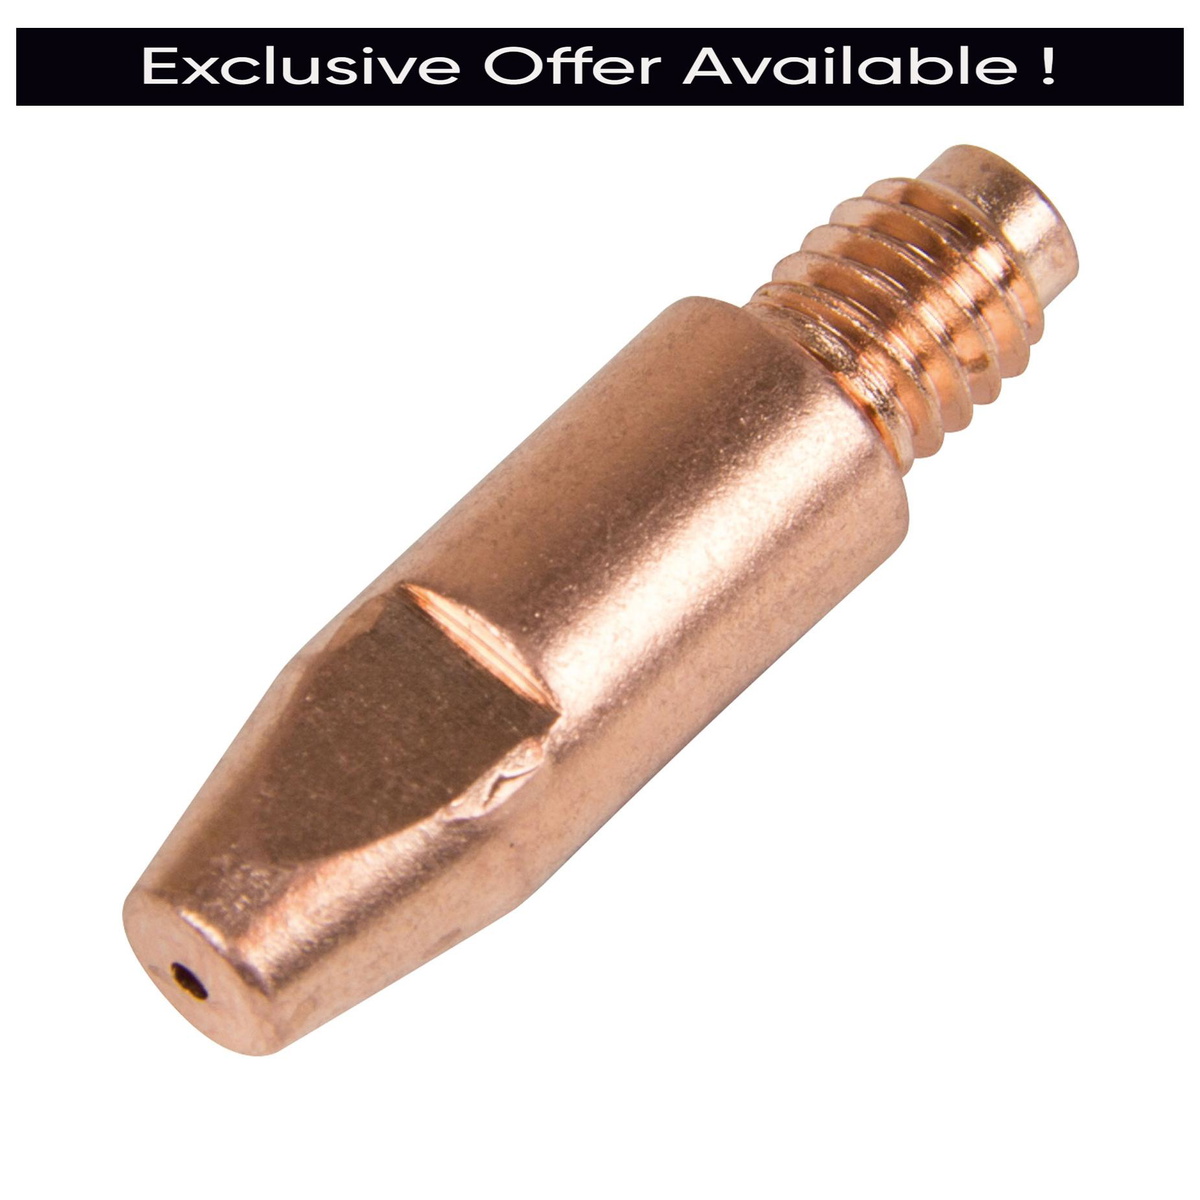
The SIP 09078 contact tip — Welding Tip M6 MIG. The SIP 1mm 25 / 36 M6 MIG Welding Tip (mig contact tip (copper contact tip)) is manufactured from high-quality copper for reliable contact with welding wire, providing a consistent welding arc in demanding applications thanks to high conductivity and high heat resistance. High-quality copper-made 1mm 25 / 36 M6 welding tip. Designed for a range of MIG welding applications. Compatible across the sip welding, sip contact tips welding range — check product specifications for exact model fit. When ordering, search under mb15 contact tip or mb25 contact tip for this and compatible alternatives.
Additional Information:
The SIP 1mm 25 / 36 M6 MIG Welding Tip is manufactured from high-quality copper for reliable contact with welding wire, providing a consistent welding arc in demanding applications thanks to high conductivity and high heat resistance.About PartsForMachines:
PartsForMachines is a premier e-commerce platform, founded in 2019 in Warwickshire, UK, specializing in aftermarket parts and services for construction, agriculture, and industrial machinery. We offer an extensive catalog of over 500,000 products. Standard delivery: 1–3 working days within UK mainland. We are proud to be an authorised distributor, giving customers extra confidence when purchasing genuine products from us. In addition, we provide a 30-day return policy for eligible items.
| ITEM NO | 09078 |
|---|---|
| Welding Tip Type | M6 MIG |
| Welding Tip Size | Ø 1.00mm |
| Suitable For | 05505 / 05510 / 05515 |
 Standard Delivery: £4.99
 Next Day Delivery Available
 Delivery Estimate: 2 to 4 working days
 Save Extra With 1 Offer
 Compare With Similar Items
Compare with Similar products
|

Welding No.2 Swaged Heavy Duty Nozzle for Oxy-Acetylene Welding, 35035, Draper
£13.54
£13.27
2% OFF
|
||||
| Technical Specification | |||||
|---|---|---|---|---|---|
| PRODUCT NUMBER | 09070 | 09080 | 35105 | 35035 | 35036 |
A. Suitable for use alongside compatible welding machines — refer to the product specifications for machine compatibility details. The key compatibility factor is the torch body — this tip fits Euro-fit torch bodies. If your MIG welder uses this torch standard, this tip will fit.
A. Yes — the SIP 09078 is bored to Ø 1.00mm. Using a tip bored to the exact wire diameter gives the best arc stability. If you're switching between wire gauges, you'll need a separate set of tips for each size.
A. A good rule of thumb is to keep a minimum of 10–20 tips per wire diameter in stock. For production welding, tips can last as little as 30 minutes of arc time before bore wear causes arc wander. The SIP 09078 comes in a pack of 10 — order several packs if you weld regularly.
A. Replace your SIP contact tip when you notice: increased spatter that doesn't improve with wire speed or voltage adjustment; the arc starts wander or becomes erratic; visible bore wear makes the wire rattle in the tip. On a Euro-fit torch, tip changes take under a minute with the right spanner.
A. These are different torch standards — they're physically incompatible with each other. MB14 is a smaller, lighter torch typically found on entry-level and compact MIG machines. MB15 (also called Binzel 15) is the most common torch in the UK on mid-range MIG welders. MB25/36 is a heavier-duty torch for higher-amperage and professional machines. The SIP 09078 is a Euro-fit tip — check your torch body before ordering.
A. Standard contact tips like the SIP 09078 are copper. Bi-metal (copper/silver alloy) tips last longer and suit aluminium wire better, but cost more. For standard mild steel MIG welding, copper tips are the right choice — replace them frequently rather than buying expensive tips and running them too long.
A. Finger-tight then a quarter turn with a spanner is sufficient. Over-tightening the SIP 09078 makes future removal difficult, especially when the tip has been welded in by spatter. Some welders apply a small smear of anti-spatter spray to the nozzle and tip thread to prevent this — it extends tip life and makes changes quicker.
A. Rapid spatter buildup usually means voltage is set too low for your wire speed, or the tip is already slightly worn and the arc is tracking back. Check your settings first. If spatter persists with new tips and correct settings, a coat of anti-spatter compound on the SIP Euro-fit nozzle before welding will dramatically reduce buildup.
A. MIG tips and nozzles are torch-specific. Check your machine's torch type — common types include MB14, MB15, MB25, and MB36. The contact tip thread size must match your torch body. The tip bore size must match your wire diameter. Using the wrong tip or nozzle will cause poor wire feed and inconsistent welds.
A. Check the torch body on your SIP MIG welder — look for the MB designation (MB14, MB15, or MB25) printed on the torch body or in your machine manual. The SIP 09078 is a Euro-fit tip. If your machine uses a Euro-fit torch, this is a direct fit. If you're unsure, the compatible machine list in the product specifications confirms which SIP welders this tip is designed for.
By sharing your email, you agree to our privacy policy & terms of service



 Question about this product? Click here